Introduction
Choosing the right panel for a kitchen is one of the most consequential decisions in any cabinetmaking project. The wrong material in the wrong location — chipboard under a sink, uncoated MDF on a door — leads to swelling, delamination and expensive repairs within two years. This guide breaks the kitchen down into three distinct zones — worktop, carcass (cabinets) and door fronts — and assigns the best panel material to each, with exact thicknesses, weights and cost trade-offs. Whether you are a professional joiner or a committed DIYer, the numbers here will help you order the right sheets before the first cut.
Worktop Panels: Density and Moisture Resistance Come First
A kitchen worktop faces daily water exposure, heat, cutting impact and abrasion. No standard MDF or plain chipboard panel meets these demands without a protective surface layer.
Compact laminate (also called solid HPL) is the professional benchmark. It is a through-coloured phenolic resin panel, typically 12–20 mm thick, with a density of 1,350–1,400 kg/m³. It is fully waterproof, chemical-resistant and requires no edge banding. Cost is high — expect €150–250/m² installed — but lifespan exceeds 15 years in commercial kitchens.
Post-formed chipboard worktops (laminate-faced particleboard) dominate the mid-market. They use a 38 mm thick MR chipboard core with a bonded laminate surface. They work well when the substrate remains dry and sealed at every cut edge. Always apply PVC or ABS edge banding and silicone sealant around sinks and hobs. Unsealed chipboard edges absorb water and begin to swell within weeks.
Solid wood and engineered wood worktops look excellent but require annual oiling and expand seasonally. They suit low-moisture areas like islands away from the sink. Thickness is typically 27–40 mm.
| Worktop Material | Thickness | Density (kg/m³) | Water Resistance | Relative Cost |
|---|---|---|---|---|
| Compact laminate (HPL) | 12–20 mm | 1,350–1,400 | Excellent | High |
| MR chipboard + laminate | 38 mm | 650–700 | Good (sealed) | Low |
| Solid oak / engineered | 27–40 mm | 600–750 | Moderate | Medium–High |
| Marine plywood | 18–25 mm | 680–720 | Good | Medium |
Cabinet Carcasses: Load, Machinability and Cost
The carcass is the hidden workhorse. It carries shelf loads, hinge loads and the weight of the worktop above. Three materials compete here.
Moisture-resistant (MR) chipboard — also sold as P3 or V313 particleboard — is the standard across European flat-pack and custom cabinetry. At 16 mm for wall units and 18 mm for base units, it holds screws adequately when a washer head or confirmat fastener is used. Density sits at 620–680 kg/m³. An 18 mm sheet (2,440 × 1,220 mm) weighs approximately 16–17 kg. Cost: €18–28 per sheet.
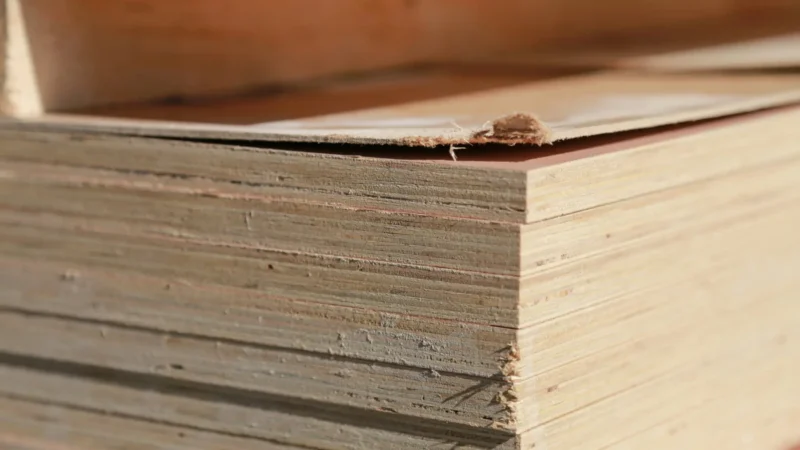
Birch plywood (BB/BB or BB/WG grade) at 15–18 mm is significantly stronger in bending and holds screws in any direction, including the edge. Density is 680–720 kg/m³. A 15 mm birch plywood sheet (2,440 × 1,220 mm) weighs around 15 kg — similar to chipboard at the same format — but the bending stiffness is 25–35% higher. Cost: €45–75 per sheet, making it roughly 40–60% more expensive than MR chipboard.
Standard MDF is not recommended for kitchen carcasses in wet zones. It holds screws poorly on the face and very poorly on the edge, and swells irreversibly when wet. Moisture-resistant (MR) MDF is an improvement, but it still absorbs more water than plywood and costs more than chipboard for equivalent performance in the carcass role.
For most kitchens, MR chipboard is the rational choice for carcasses. Upgrade to birch plywood for larder units carrying over 50 kg per shelf, or for any unit adjacent to a dishwasher or under-sink location.
Before cutting, use the Offcut panel cut optimisation tool to lay out carcass parts across full sheets — minimising waste on expensive birch plywood can save two to three full sheets on a 10-unit kitchen.
Door Fronts and Facades: Appearance, Stability and Weight
Kitchen doors are the only part of the kitchen the user touches and sees every day. The material choice affects finish quality, long-term stability and the structural load on the hinges.
MR MDF at 18–22 mm is the dominant material for painted kitchen doors. Its consistent, grain-free surface takes primer and paint with minimal preparation. It machines cleanly for routed ogee and shaker profiles. Density: 700–780 kg/m³. An 18 mm MDF door blank (700 × 400 mm) weighs approximately 4 kg — manageable for standard soft-close hinges. At 22 mm for larger panels, check hinge load ratings carefully.
Real-wood veneer plywood suits contemporary and Scandinavian aesthetics. A 3–4 mm oak, walnut or birch veneer is factory-pressed onto a plywood core. The panel is more dimensionally stable than solid timber and lighter than solid MDF at equivalent thickness. Cost is higher than MDF but lower than solid wood.
Thermofoil (vinyl-wrapped MDF) dominates entry-level kitchens. A PVC film is vacuum-pressed onto an MDF core. The result is seamless, easy to clean and moisture-tolerant at the face — but the film can peel at edges if exposed to steam over time.
Solid timber doors (stile-and-rail construction) are the premium category. They require a floating panel design to accommodate seasonal wood movement. Weight is significant — a 22 mm solid oak door (700 × 400 mm) can weigh 5.5–6.5 kg. Always verify hinge capacity when specifying solid wood doors.
| Door Material | Typical Thickness | Surface Finish | Moisture Risk | Weight (700×400 mm) |
|---|---|---|---|---|
| MR MDF | 18–22 mm | Paint, lacquer | Low–Moderate | ~4.0–4.8 kg |
| Veneer plywood | 18 mm | Natural wood, oil | Low | ~3.5 kg |
| Thermofoil MDF | 18 mm | Vinyl wrap | Low (face) | ~4.0 kg |
| Solid timber | 20–25 mm | Oil, lacquer | Moderate | ~5.5–6.5 kg |
The cumulative weight of doors across a full kitchen fit-out is rarely calculated in advance. A kitchen with 20 door fronts averaging 4 kg each adds 80 kg of load to hinges and carcass fixings. Use the wood panel weight calculator to total the door weight before ordering hardware.
Conclusion
No single panel material wins across all three kitchen zones. MR chipboard is cost-effective and sufficient for most cabinet carcasses. Compact laminate or sealed post-formed chipboard handles worktops. MR MDF excels for painted door fronts. Birch plywood justifies its premium cost in high-load or high-moisture carcass positions.
The key discipline is being granular: specify the right panel for each function, calculate the weight of every component, and optimise your sheet layout before ordering. A full kitchen fit-out in plywood and MDF can involve 30–50 full sheets — poor layout planning wastes €300–800 in material alone.
Start your cut list now with the Offcut panel optimisation tool and reduce waste before you reach the saw.